Insulation & sheathing

Cable Extrusion Lines

Insulation and sheathing lines for power, building, solar and data cables, plus silicone, fluoropolymer and foamed-insulation applications. Select the process around the compound and cable construction.

Explore the selection guide
Ultra-fine fluoropolymer wire extrusion line

Choose the equipment for your operation

Insulation and sheathing lines for power, building, solar, data and specialty cable applications.

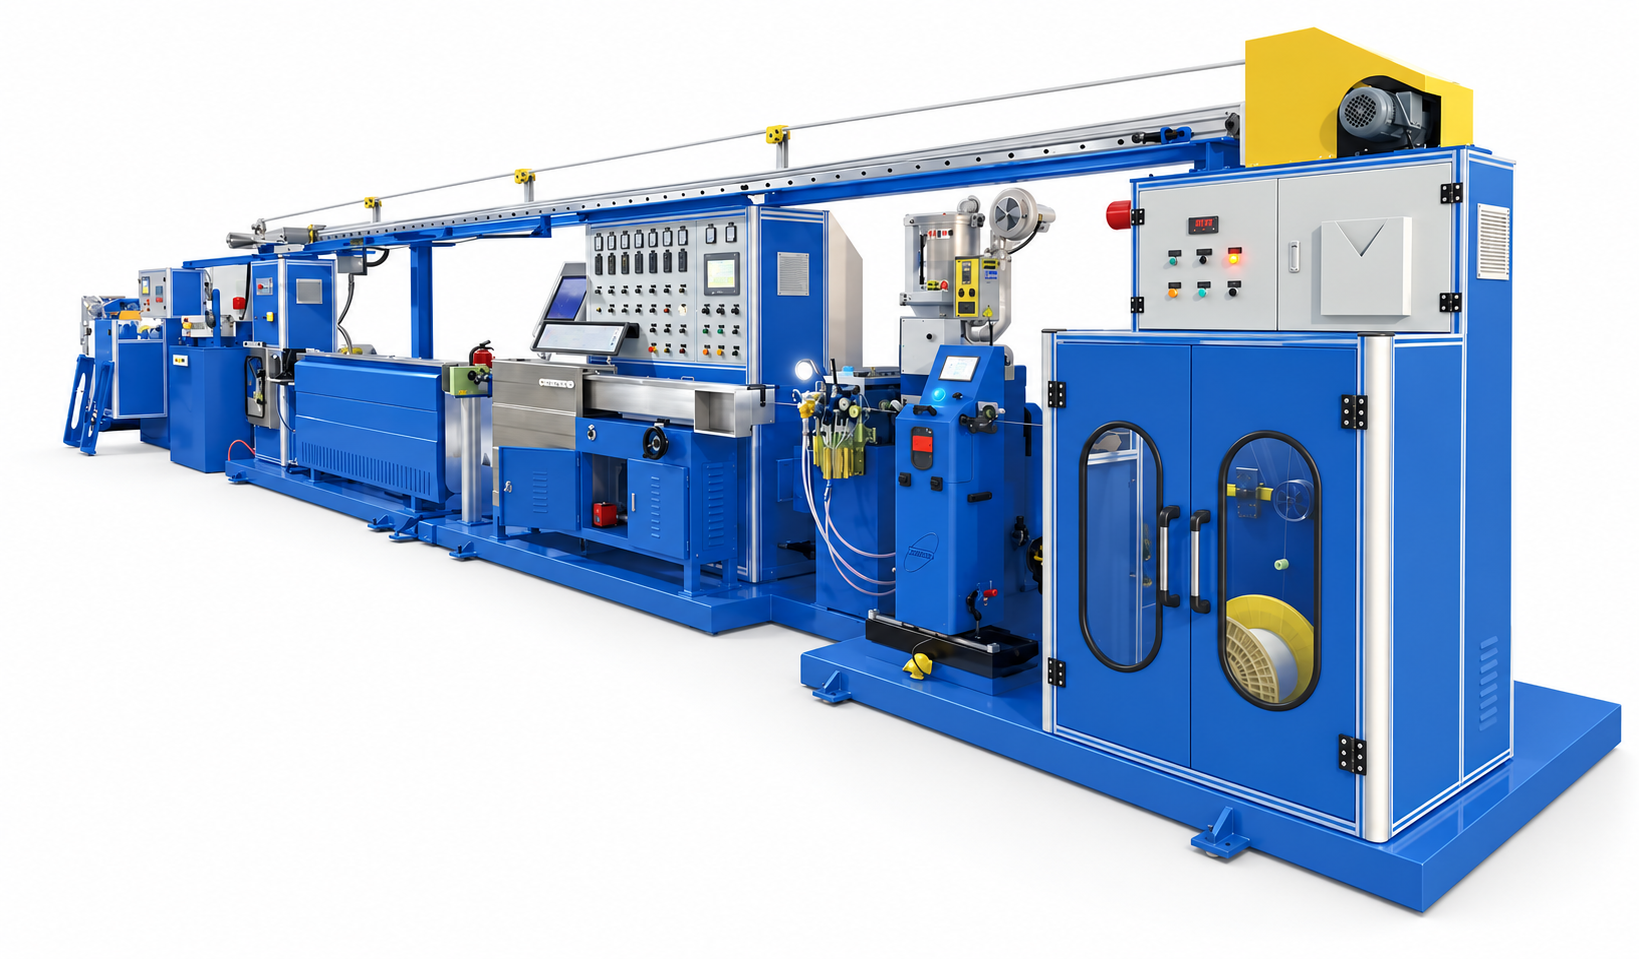
Cable Extrusion catalogue equipment example
Insulation & sheathing

Start with what the machine needs to do.

Material entering the machine
Conductor or assembled cable core
Required result
Insulated wire or jacketed cable

Match the working range, material handling and controls to this operation.

Power, building & new-energy linesCore insulation and cable sheathing

Confirm before selectionMaterial grade, conductor or core diameter, wall thickness and output.

Photovoltaic cable linesSolar cable insulation and sheath processes

Confirm before selectionCable structure, compound specification and layer arrangement.

Silicone & fluoropolymer linesSpecified specialty insulation materials

Confirm before selectionMaterial processing requirements, wire size and associated equipment.

Physical & chemical foaming linesFoamed insulation for specified cable designs

Confirm before selectionDielectric construction, material, dimensions and process requirements.

Which situation matches your project?

Open the operation you need, then review its configuration inputs.

Cable Extrusion
Cable Extrusion · catalogue equipment example
Insulating a conductorThe required layer is applied directly around an individual conductor.
Review together
Review compound grade, incoming diameter, layer thickness, finished diameter and in-line inspection.
Next decision
Provide the core drawing and the smallest and largest planned conductor sizes.
Sheathing an assembled cableA prepared cable core needs its outer jacket.
Review together
Review core dimensions, jacket compound, layer thickness, haul-off, cooling and reel handling as one line.
Next decision
Provide the core and finished-cable dimensions with the required package.
Using a specialty material or dielectricThe design calls for silicone, fluoropolymer or a foamed layer.
Review together
Review the material process and layer construction before selecting the screw, head and supporting equipment.
Next decision
Provide the compound specification and identify any required treatment or validation.
When the scope changes

Insulation and sheathing use different incoming products. Compound-specific curing, cross-linking, shielding and final cable testing need an explicit scope; they are not established by choosing an extruder size.

Compare reference configurations

Check the differences that matter to your product. Final selection follows a technical review.

Power cable insulation & sheathing

2026 catalogue · p. 23

Choose two models to compare.

PY-Φ90 compared with PY-Φ100
SpecificationPY-Φ90PY-Φ100
Screw Ø (mm)90100
Screw L/D25:125:1
Extrusion (kg/h)300350
Wire-size range Ø (mm)5–355–50
Add a model to your brief

The catalogue lists PVC, XLPE and low-smoke halogen-free applications for this family. Compound processing and any additional treatment require confirmation.

View all reference models
All catalogue reference models for Power cable insulation & sheathing
ModelScrew Ø (mm)Screw L/DExtrusion (kg/h)Wire-size range Ø (mm)
PY-Φ909025:13005–35
PY-Φ10010025:13505–50
PY-Φ12012025:140010–80
PY-Φ15015025:160020–200

New-energy cable extrusion

2026 catalogue · p. 22

Choose two models to compare.

PY-Φ70 compared with PY-Φ90
SpecificationPY-Φ70PY-Φ90
Screw Ø (mm)7090
Screw L/D25:125:1
Extrusion (kg/h)100200
Conductor area (mm²)1.5–1010–35
Add a model to your brief

These are a separate family: the same screw diameter does not imply the same output as the power-cable line. Material and conductor construction determine the final selection.

View all reference models
All catalogue reference models for New-energy cable extrusion
ModelScrew Ø (mm)Screw L/DExtrusion (kg/h)Conductor area (mm²)
PY-Φ707025:11001.5–10
PY-Φ909025:120010–35
PY-Φ11011028:130035–95
PY-Φ13013028:145095–240

Catalogue figures are reference values. Material, product dimensions and the agreed configuration determine operating output and the final technical specification.

What determines the configuration?

Review the choices behind the equipment package.

Cable Extrusion
Catalogue equipment example; configuration follows your product.
Start with the compound

PVC, LSZH, silicone and fluoropolymers require their own processing review. Confirm the compound grade and material treatment before choosing the screw, head and downstream equipment.

Separate insulation and sheathing

Insulating an individual conductor and sheathing an assembled cable use different inputs. Provide the incoming diameter, layer thickness and finished diameter for each operation.

Balance the whole line

Extruder capacity alone does not establish finished-cable output. Review cooling, haul-off, inspection and take-up against the same cable and material specification.

Check the connections around the machine.

Input, equipment and output must work as one connected process.

Incoming materialConductor or assembled cable core
Cable Extrusion
Cable Extrusion
Required outputInsulated wire or jacketed cable
Incoming product to pay-off

Confirm conductor or assembled-core dimensions, reels, loading weight and tension requirements.

Extrusion to downstream equipment

Review the same product and output basis for cooling, haul-off, measurement, spark testing and take-up.

Materials to the factory

Identify feeding, drying, cooling utilities and any separate treatment required by the actual compound.

From this operation to your production line.

See the role of this equipment in each cable project, then open the complete route.

Photovoltaic cable extrusion line

Solar Cable

Apply the specified insulation and sheath layers for solar cable.

Confirm firstConfirm compounds, layer arrangement and any separately required material treatment.

Power-cable extrusion line

Power & Building Cable

Insulate conductors or sheath assembled power-cable cores.

Confirm firstDefine each operation separately with its input diameter, compound and layer thickness.

Extrusion equipment example

LAN & Data Cable

Apply core insulation or the finished LAN cable jacket.

Confirm firstThe shown line is an example; confirm material and solid or foamed construction for the selected process.

Ultra-fine fluoropolymer extrusion line

USB & Data Cable

Review core insulation and jacket processes for the specified data cable.

Confirm firstThis photograph shows a fluoropolymer line; the required equipment depends on the actual compound.

Cable extrusion equipment example

Power Cord

Apply insulation to the cord conductors and a sheath where specified.

Confirm firstConfirm round or flat geometry and compounds. The image is a line example, not a fixed cord configuration.

Extrusion equipment example

Coaxial Cable

Apply the specified dielectric or the outer coaxial cable jacket.

Confirm firstReview solid or foamed dielectric separately; the image does not establish the final dielectric configuration.

Define your equipment package

Agree the main machine and supporting items together before comparing proposals.

Specify in the equipment list

  • Pay-off and conductor or cable-core handling
  • Extruder, screw and head for the selected material
  • Cooling, haul-off and take-up arrangement
  • Specified diameter measurement and spark testing

Confirm the related requirements

  • Material drying, feeding and plant cooling utilities
  • Cross-linking, curing or other material-specific treatment
  • Finished-cable testing and applicable product requirements

Compare the proposal, not only the model.

Is the quotation based on the same compound, layer and finished cable?

Use the same product and scope when comparing suppliers.
DecisionWhat to checkWhat to request
Material & layerSeparate insulation from sheathing. Identify the compound grade, input product, layer thickness and finished dimensions.A cable/material schedule tied to the proposed screw, head and line arrangement.
Finished layerAgree how dimensions, concentricity where relevant, surface and in-line checks will be assessed on your material.Trial conditions, measuring/inspection scope and the acceptance points to agree.
Supporting lineCheck pay-off, cooling, drying, haul-off, accumulation and take-up together with the extruder.A complete equipment list and line/interface drawing with supply boundaries.
Output & specialist processesCompare output on the same product. Any curing, cross-linking or other material treatment requires a separately defined scope.Product-specific operating assumptions and a list of external processes or equipment.

What changes the quotationCompound and layer requirements, screw/head arrangement, tooling, cooling, in-line checks, haul-off and take-up change the package. Mark tooling, supporting units, site works and services as included, optional or buyer-supplied before comparing prices.

Define a useful equipment trial.

Agree the representative product, incoming material, setup, run conditions, measurements and records before the trial. Confirm the acceptance criteria together; a catalogue maximum is not a guaranteed result for every product.

Prepare your selection requirements

Cable dimensions

Input diameter, insulation or sheath thickness and finished diameter.

Compound

Material type and grade, layer count and specialty processing needs.

Production mix

Target products, output expectations, colors and changeover needs.

Supporting equipment

Pay-off, cooling, haul-off, spark testing, diameter measurement and take-up.

Equipment questions

Can one line produce every cable material?

A line is selected for a defined material and product range. Conventional thermoplastics, silicone, fluoropolymers and foaming applications need their own technical review.

Is a published speed the output for my product?

Actual production depends on the product, compound, dimensions and complete line configuration. Confirm output against the intended cable rather than a standalone machine figure.

Can inspection equipment be included?

Spark testers and laser diameter gauges are included in the catalog’s supporting equipment. Their role and position should be agreed for the selected process.

Does a larger screw always give a better line?

No. The material, required output, cable dimensions and operating range should determine the screw and line configuration. The smallest and largest products in your planned range both need review.

What affects the price of a cable extrusion line?

The material system, screw and head, number of layers, reel handling, cooling length, controls and inspection equipment affect the quotation. Compare the complete equipment list and supply responsibilities.

Your Project Brief

Share the cable you want to make and the scope of your project.

Sample site: prepare and download a project brief locally. No inquiry is sent.